Draw ratio is one of the most consequential variables in vacuum forming, and one of the least discussed in equipment selection conversations. It determines whether a part can be produced as designed, which materials can produce it, and how wall thickness will distribute across the finished component.
Getting draw ratio wrong doesn’t usually produce obvious failures at forming. It produces parts that are technically formed but structurally weak at the base corners, dimensionally inconsistent from cycle to cycle, or prone to cracking under load in service. Understanding what draw ratio means, how it behaves across different materials, and what it demands from equipment and tooling helps avoid those outcomes before they become production problems.
How Draw Ratio Is Defined
Draw ratio is the relationship between the depth of a formed part and its smallest horizontal inside dimension. A part that is 10 inches wide and 5 inches deep has a draw ratio of 0.5:1. A part that is 4 inches wide and 8 inches deep has a draw ratio of 2:1.
The significance of this ratio is in what it tells you about how far the material has to stretch during forming. At a low draw ratio, the sheet travels a short path from the clamp frame to the base of the mold. At a high draw ratio, the material must stretch considerably to fill the mold geometry. That stretching thins the sheet — and the thinning isn’t uniform across the part.
What Actually Happens to Wall Thickness During Deep Draws
When a thermoplastic sheet is drawn over or into a mold, the material stretches to follow the mold surface. The areas that contact the mold surface first stop moving. The areas still bridging open space continue to stretch. At the deepest point of a high-ratio draw, material can thin to a fraction of its original gauge.
This thinning follows predictable patterns depending on tooling orientation. With male tooling, where the sheet is drawn over the mold, the thinnest areas are typically the base corners where the sheet transitions from sidewall to bottom. With female tooling, where the sheet is drawn into the mold cavity, thinning concentrates at the deepest corners of the cavity.
The practical consequence is that two parts formed from the same sheet gauge can appear visually identical while having very different wall thickness profiles. A well-managed deep draw maintains acceptable thickness throughout. A poorly managed deep draw produces a part that fails at the base corners under stress regardless of how it looks at release.
Practical Draw Ratio Limits by Material
Every thermoplastic has a practical maximum draw ratio where consistent, acceptable parts can still be produced. Exceeding that limit produces thinning, surface defects, or tears. The limits vary significantly by material ductility and forming temperature range.
| Material | Typical Practical Draw Ratio | Notes |
|---|---|---|
| ABS | 1:1 to 1.5:1 | Good ductility; responds well to plug assist beyond 1:1 |
| HIPS | 0.75:1 to 1:1 | Less ductile than ABS; tighter practical limit on deep draws |
| Acrylic | 0.5:1 to 0.75:1 | Lower ductility; cracks under excessive stretch if temperature is off |
| HDPE | 1.5:1 to 2:1 | High ductility; handles deep draws better than most amorphous plastics |
| Polycarbonate | 1:1 to 1.5:1 | Requires proper pre-drying; performs well with correct process setup |
| PETG | 1:1 to 1.5:1 | Good formability; more forgiving than PC for deep draw applications |
These are general production ranges. Actual performance depends on sheet grade, heater type, forming temperature, vacuum system capacity, and tooling geometry. The Society of Plastics Engineers publishes material-specific forming guidelines that are useful when pushing toward the upper limits of draw ratio for a given thermoplastic. The vacuum forming material selection guide covers how material properties factor into production decisions including draw depth capability.
How Plug Assist Changes What’s Achievable
For parts where the required draw ratio exceeds what vacuum alone can produce acceptably, plug assist is the primary solution. A plug assist is a mechanical tool, typically made from syntactic foam or another low-conductivity material, that physically pre-stretches the sheet into the mold cavity before vacuum is applied.
By distributing material more evenly into the mold before the vacuum draw begins, plug assist reduces the concentration of thinning at the base corners. Parts that would thin unacceptably under vacuum alone can be produced to acceptable wall thickness profiles with plug assist. It adds tooling complexity and cycle time, but for applications where draw ratio requirements are non-negotiable, it’s the standard production solution.
What Vacuum System and Machine Configuration Mean for Deep Draw Parts
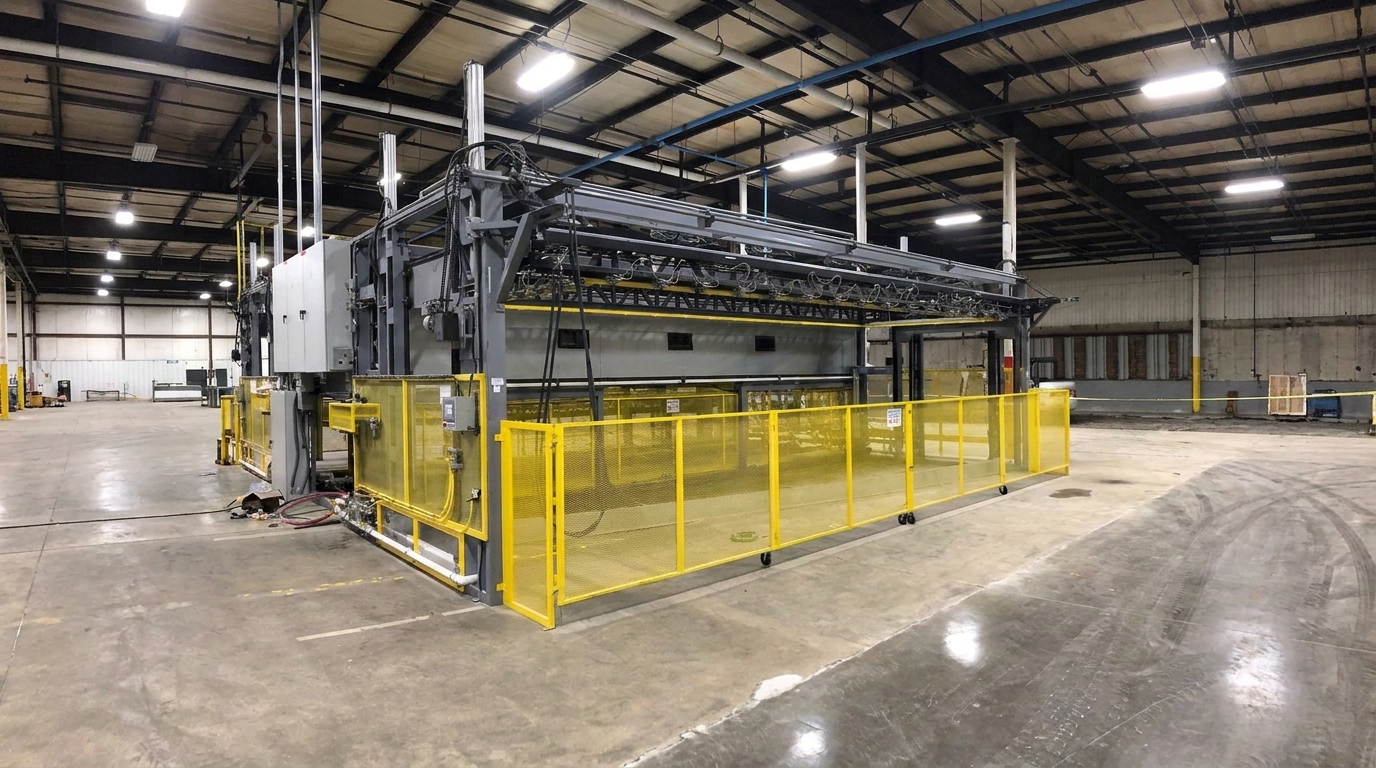
Draw ratio isn’t purely a material and mold problem. The vacuum system on the forming machine plays a direct role in how deep draws perform. A vacuum system that can’t pull the sheet quickly against the mold before it begins to cool will produce inconsistent wall thickness even on draws that are nominally within material limits.
The relationship between station configuration and deep draw consistency is significant. Dual-station machines allow longer, more controlled heat soak before the forming cycle begins, which produces more uniform temperature distribution through the sheet thickness at the point of draw. More uniform temperature at draw means more consistent material distribution into deep geometry. The full comparison is covered in the single-station vs dual-station guide.
Vacuum pump sizing also directly affects deep draw performance. Undersized pumps produce slower draw speeds, more material cooling during the forming cycle, and greater variation in wall thickness from part to part. The vacuum pump sizing guide covers how to match pump capacity to the surface area and draw depth requirements of a given application.
Starting at Design Rather Than Fixing at the Machine
The most common mistake in production planning is designing a part with a draw ratio that exceeds material limits, then trying to solve the resulting quality problems at the machine rather than at the design stage. Adjusting forming temperature, vacuum timing, and cycle parameters can improve results at the margin. They can’t overcome a draw ratio that fundamentally exceeds what the material can handle.
Getting draw ratio into spec during part design, selecting a material that can handle the required depth, and specifying a machine with adequate vacuum capacity and heater control for the part geometry produces a process that runs consistently from day one. The vacuum forming machine selection guide addresses how to evaluate equipment capability for your application profile, including draw depth requirements. If you’re working through a part with specific deep draw requirements and want to evaluate machine configuration, Belovac’s team can help match the right machine to your production needs.